Air Compressor Servicing Aberdeen
A service visit should protect production, not merely satisfy a calendar entry. Design Air, an Atlas Copco Premier Distributor in Scotland, provides planned maintenance, breakdown support and service contracts for industrial sites across Aberdeen and the North East.
We base the scope on equipment condition, operating hours, air quality, redundancy and the production cost of losing pressure. Aberdeen quotations include agreed attendance terms and northern travel, so facilities and procurement teams know what is covered before work begins.
The Production Problems Servicing Must Control
Compressed air faults rarely remain confined to the compressor room. Falling pressure slows pneumatic tools and actuators. Wet air affects instruments, valves and process quality. Repeated high-temperature shutdowns interrupt production and shorten component life.
The purpose of planned servicing is to identify the condition causing the change before it becomes an unplanned stoppage.
Downtime Depends on the Site Configuration
A fabrication workshop with a standby compressor can tolerate a different repair window from an offshore supply facility running one duty machine. The service scope must account for which processes stop first, whether standby equipment starts automatically and how much useful demand the receiver can support.
An air receiver can bridge a short demand peak, but it cannot increase the compressor’s continuous free air delivery. If average demand exceeds available capacity, more receiver volume only delays the pressure fall. The underlying answer may be leak reduction, control changes or additional generation capacity.
Small Restrictions Create Measurable Costs
An inlet filter or oil separator can appear intact while imposing a substantial pressure loss. Atlas Copco states that an additional 25 mbar pressure drop at the air inlet can reduce free air delivery by 2%. A 1 bar pressure drop across a saturated or unsuitable oil separator can increase electrical power consumption by 7%, according to its compressor parts guidance (atlascopco.com).
The inlet restriction reduces the mass of air reaching the compression element. Separator resistance forces the element to operate at a higher internal pressure to maintain the required network pressure. The site therefore receives less useful air for the electricity consumed.
If point-of-use pressure remains low after the compressor has been checked, our guide to air compressor pressure problems explains how to distinguish a supply restriction from leakage or increased plant demand.
Aberdeen Conditions Affect the Inspection Scope
Cold external pipework, wind-driven moisture and salt-laden air can change the failure pattern at Aberdeen industrial sites. Intake filtration, cooler surfaces, electrical enclosures, condensate drains and exposed distribution equipment may need closer inspection than equivalent components inside a heated plant room.
Scope Available for an Aberdeen Site
We can build the service around the installed equipment and production risk rather than applying one checklist to every compressor. The initial equipment register should include compressors, dryers, filters, drains, receivers, controllers and relevant distribution components.
| Service Element | Work Undertaken | Useful Output |
|---|---|---|
| Planned servicing | Manufacturer-scheduled oil, filter, separator and consumable work | Service record and next-due schedule |
| Condition inspection | Temperatures, pressures, differential pressures, cooling and drain checks | Condition report with developing defects |
| Fault diagnosis | Controller history, pressure testing and supply-side or demand-side isolation | Identified fault and repair scope |
| Energy assessment | Logged flow, power, pressure and leak investigation | Baseline and ranked efficiency actions |
| Compliance support | Installation review against the Written Scheme and safe operating limits | Items requiring competent-person review |
| Breakdown support | Remote triage, agreed attendance and repair planning | Defined response route and required parts |
Planned Maintenance and Fault Diagnosis
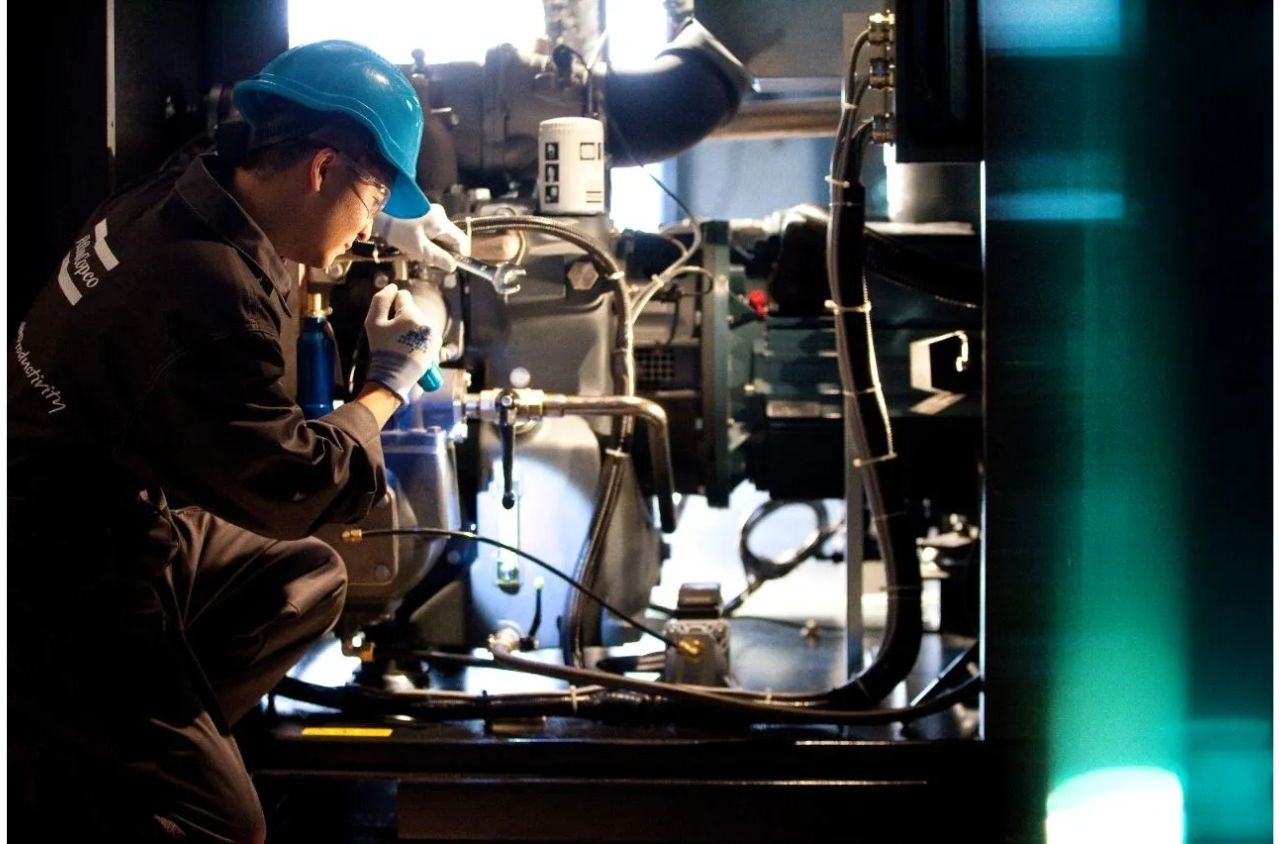
A planned visit should record run hours, loaded hours, controller warnings, operating temperature, inlet restriction, separator differential pressure and dryer performance. The engineer should compare these readings with the machine’s previous condition and model-specific limits.
A fault visit starts with the symptom and operating state. Low pressure, high temperature, oil carryover and repeated loading cycles have several possible causes. The checks described in common air compressor problems and how to fix them help site teams record useful evidence without assuming the first alarm identifies the root cause.
Moisture Control and Air Quality
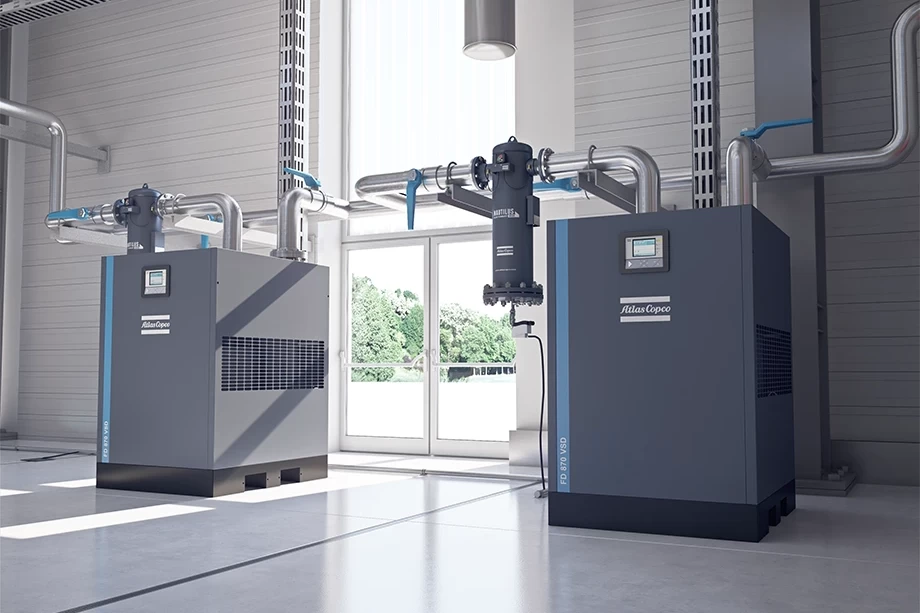
A refrigerant dryer commonly produces a pressure dew point of approximately +3°C, which corresponds to ISO 8573-1 water Class 4. That can be suitable for general industrial air kept within a heated internal network.
It is not sufficient when the pipework can fall below the dryer’s pressure dew point. Condensation then forms downstream even though the dryer is operating correctly. Where distribution pipework crosses unheated external areas during an Aberdeen winter, or where the process requires much drier air, a desiccant dryer becomes necessary. Typical specifications range from -40°C to -70°C PDP, subject to the required air-quality class and operating conditions. The distinction is explained in this ISO 8573-1 air-quality guidance (airbestpractices.com).
Energy Assessment Before Replacement
Replacement should begin with a measured baseline. An ISO 11011 AIRScan can log flow, power and pressure across production shifts, revealing whether energy is being lost through leakage, excessive discharge pressure, poor sequencing or unsuitable equipment.
Atlas Copco reports that a comprehensive compressed air energy audit (atlascopco.com) can identify savings equivalent to 10% to 25% of annual power costs through measures such as leak remediation and pressure optimisation. The result depends on the starting condition of the site.
Legacy fixed-speed equipment should not be replaced on published savings figures alone. Atlas Copco states that VSD+ compressors can reduce energy consumption by up to 50% in suitable variable-demand applications (atlascopco.com). The drive reduces motor speed when demand falls, avoiding extended unloaded running. A stable base-load duty may still favour a fixed-speed machine, so logged demand must govern the decision.
Evidence Behind the Service
An Aberdeen buyer needs evidence that the provider can work to the installed machine’s technical requirements, supply traceable parts and produce a useful service record.
Premier Distributor Status
Design Air’s Atlas Copco Premier Distributor status gives our engineering team access to the manufacturer’s technical information, genuine components and service procedures. Factory-trained engineers work to the relevant model schedule rather than substituting a generic oil-and-filter visit.
Genuine parts are particularly important when fit, filtration performance or pressure drop affects compressor efficiency. The quotation should identify the planned parts, labour and waste handling so procurement can compare like-for-like scopes.
Reports That Support Decisions
A useful report records measurements and actions, not just a completed checklist. It should show operating pressures, temperatures, differential pressures, controller warnings, dryer dew point and defects requiring follow-up.
Where a repair is recommended, the report should distinguish between an immediate production risk, planned remedial work and an efficiency opportunity. That separation helps the site decide what must be done now and what belongs in the next maintenance or capital budget.
Building an Accurate Aberdeen Quotation
We start by establishing what is installed, how it operates and what happens if it stops. A photograph of the data plate is helpful, but it does not replace an equipment schedule or production-risk discussion.
For an accurate quotation, provide:
- The Aberdeen site postcode and access arrangements
- Compressor, dryer and receiver makes, models and serial numbers
- Current run hours, loaded hours and controller warnings
- Previous service records and known repairs
- Operating pressure and required point-of-use pressure
- Production hours, shift pattern and periods of variable demand
- Required particle, water and oil purity classes
- Pipework sections exposed to outdoor or unheated conditions
- Standby capacity and temporary-air requirements
- Current faults, recent alarms and acceptable attendance window
Site Assessment
Our engineer confirms the equipment register and inspects the compressor room, treatment equipment and relevant distribution network. Where the symptoms are intermittent, the assessment may include pressure, flow, power or dew-point logging across a representative production period.
The assessment determines whether the quotation requires routine servicing, immediate repairs, an energy audit, air-quality testing or a separate compliance review. It also identifies any planned shutdown or permit requirements before attendance.
Northern Travel and Attendance Terms
Aberdeen work is quoted for the actual site rather than being placed under a Central Belt response-time assumption. The quotation states travel, planned attendance, breakdown contact arrangements and any agreed priority response.
Critical sites should specify the production consequence, redundancy available and maximum acceptable interruption. Those details influence engineer allocation, parts holding and whether temporary compressed air should form part of the contingency plan.
Service Intervals and Operator Limits
Service intervals depend on the exact compressor model, lubricant, controller data, ambient condition and duty cycle. Calendar age matters alongside operating hours because filters, seals and fluids can deteriorate even when annual use is low.
Typical rotary screw reference points may include:
| Running Hours | Possible Reference Activity |
|---|---|
| 500 | Initial or minor checks |
| 2,000 | Air, oil or panel filter changes |
| 4,000 | Oil separator replacement |
| 8,000 | Fluid change and valve inspection |
| 50,000 to 60,000 | Airend condition review or overhaul |
These are planning references, not a universal service schedule. The current model-specific manufacturer schedule and the site’s operating conditions always govern. A dusty intake, restricted ventilation, high loaded hours or repeated high-temperature operation may justify earlier intervention.
What Can Site Operators Check Safely?
Operators can record oil level where the manufacturer provides a safe viewing method, controller temperatures, pressure, dew point, drain operation, loaded hours, unusual noise and visible leakage. Trend data is more useful than an isolated reading because it shows whether the machine is moving away from its normal operating condition.
Routine observation is not authority to open pressurised equipment, remove guards, adjust safety devices or carry out internal work. Isolation, depressurisation and maintenance must follow the manufacturer’s procedure and the site’s safe system of work.
Servicing and PSSR Compliance
Routine servicing does not replace statutory examination. The Pressure Systems Safety Regulations 2000 require qualifying systems to have a suitable Written Scheme of Examination before use and to be examined in accordance with that scheme. The Health and Safety Executive’s PSSR guidance (hse.gov.uk) explains the duties and competent-person requirements.
A service visit can identify damaged components or installation changes that need review. Altering a receiver, protective device, safe operating limit or relevant pipework may require the Written Scheme to be reconsidered before the system returns to normal operation.
Selecting the Right Service Agreement
A suitable agreement reflects the consequence of failure. A site with in-house engineering support may need scheduled parts, planned labour and condition reporting. A production-critical facility may require broader repair coverage, priority breakdown terms and planned overhaul provision.
What the Agreement Should Define
The agreement should define:
- Included equipment and service intervals
- Parts, lubricants, labour and waste handling
- Breakdown contact and Aberdeen attendance terms
- Reporting, controller data and condition monitoring
- Repairs or overhauls included in the price
- Exclusions and quotation approval limits
- Energy and compliance work supplied separately
- Planned shutdown and temporary-air responsibilities
The lowest annual price can represent the highest production exposure if travel, breakdown labour, major parts or diagnostic work are excluded. Compare the operational scope and reporting evidence before comparing totals.